

Hopper - The Online Quality Optimizer
Automatically generated suggestions for parameter optimization help you reduce scrap and cycle time in the injection molding process.

Reduce Scrap in the Injection Molding Process - with a Hopper
Our AI models continuously learn the optimal process parameters to adapt the production process to changing conditions at any time.
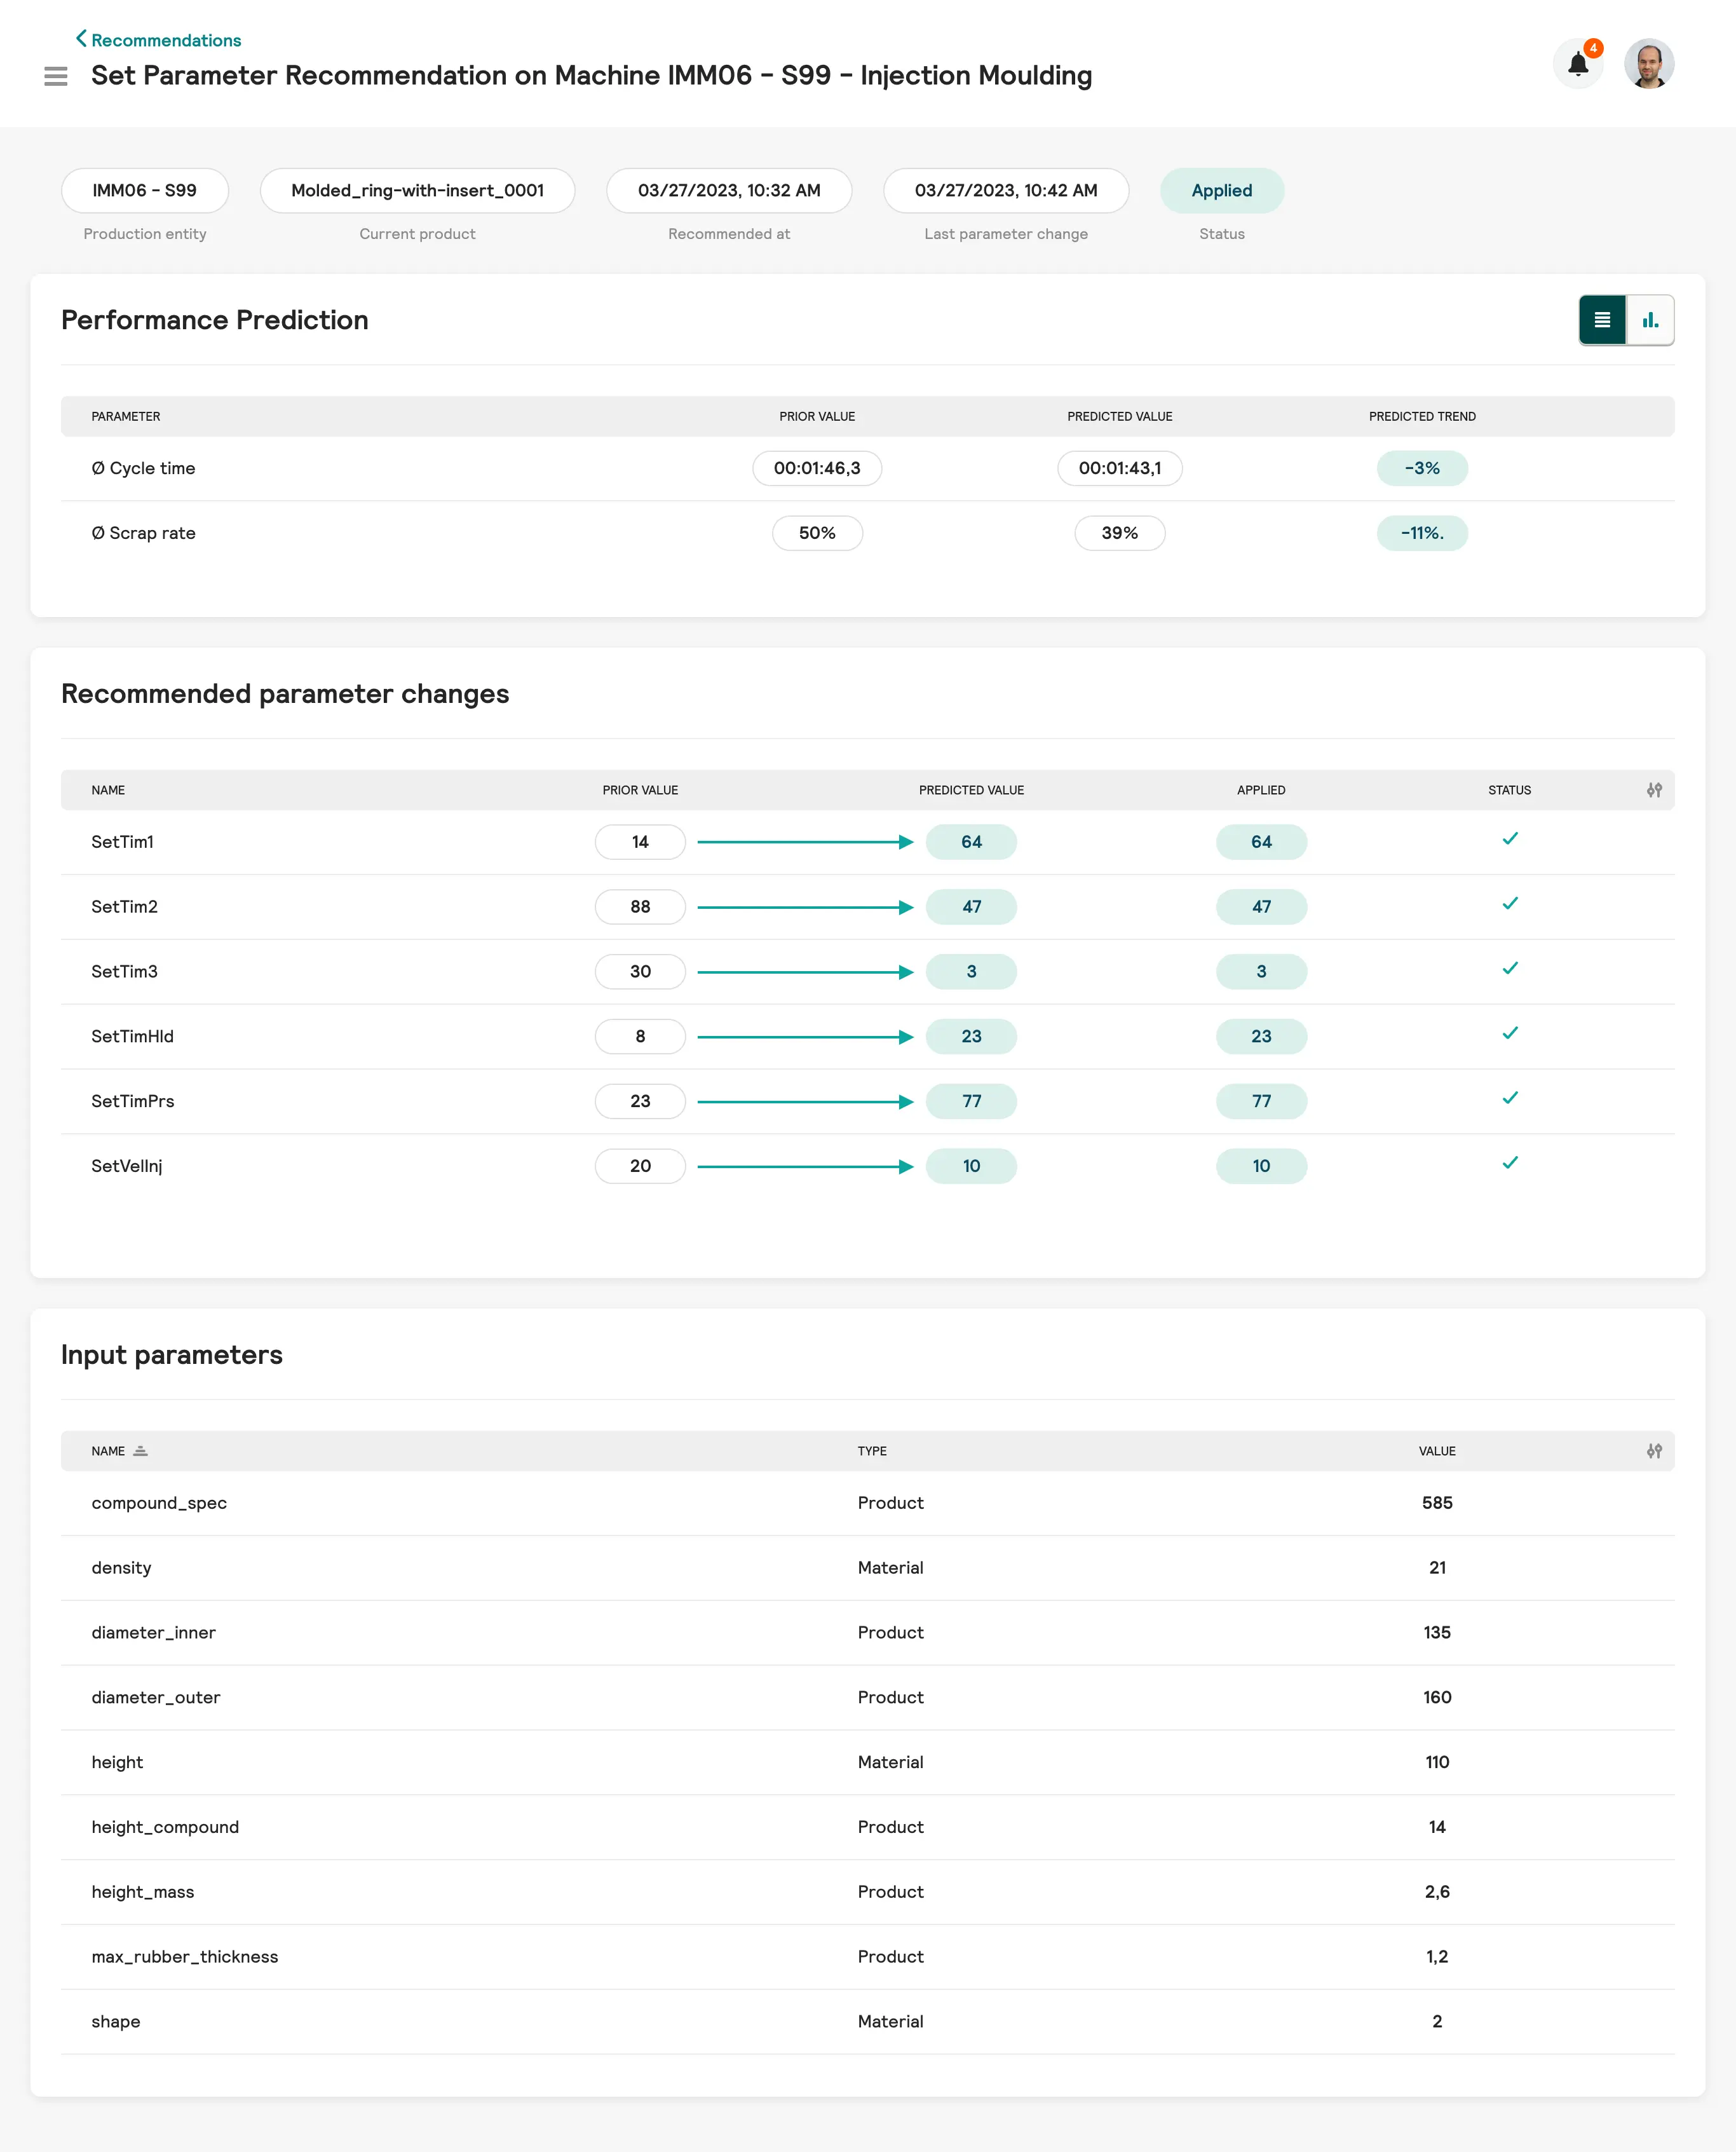
Have parameter adjustments automatically suggested to you
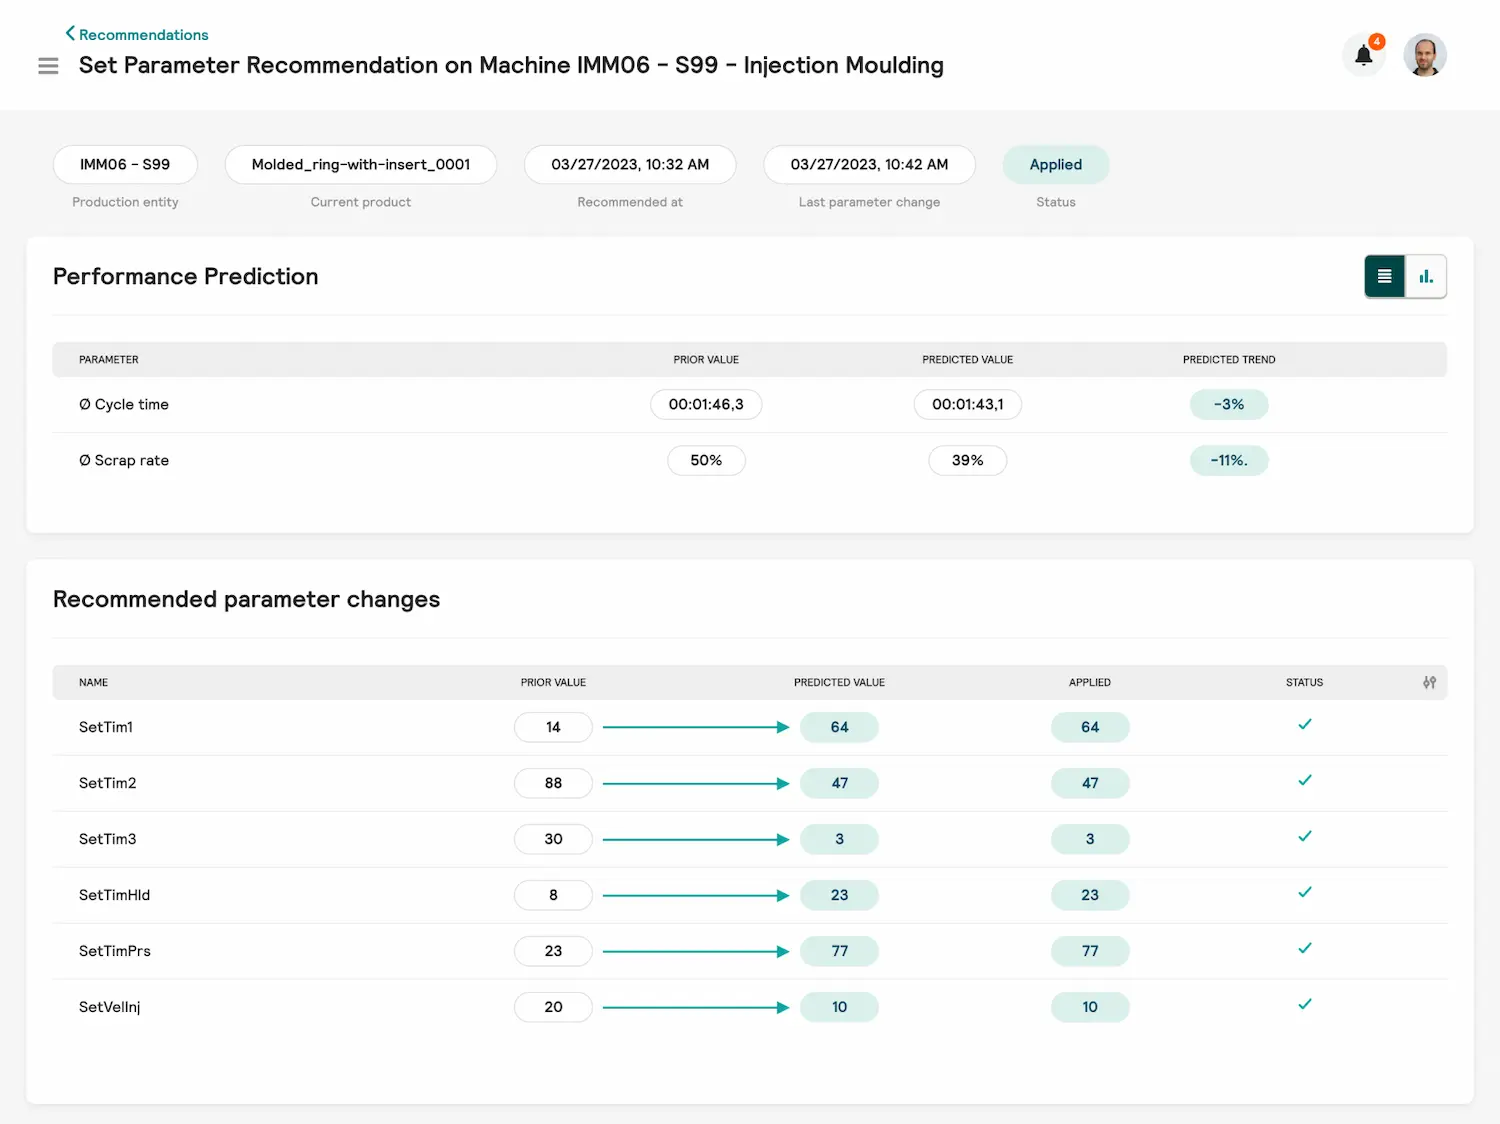
Hopper continuously analyzes the influencing variables of the injection molding process and suggests situational adjustments to set parameter - with the aim of keeping scrap and cycle time as low as possible.
- Consideration of material, process and environmental data
- Receiving recommendations in a browser or on a mobile device via push notifications

= Continuous reduction and stabilization of scrap rate and cycle time
Our AI models are continuously learning
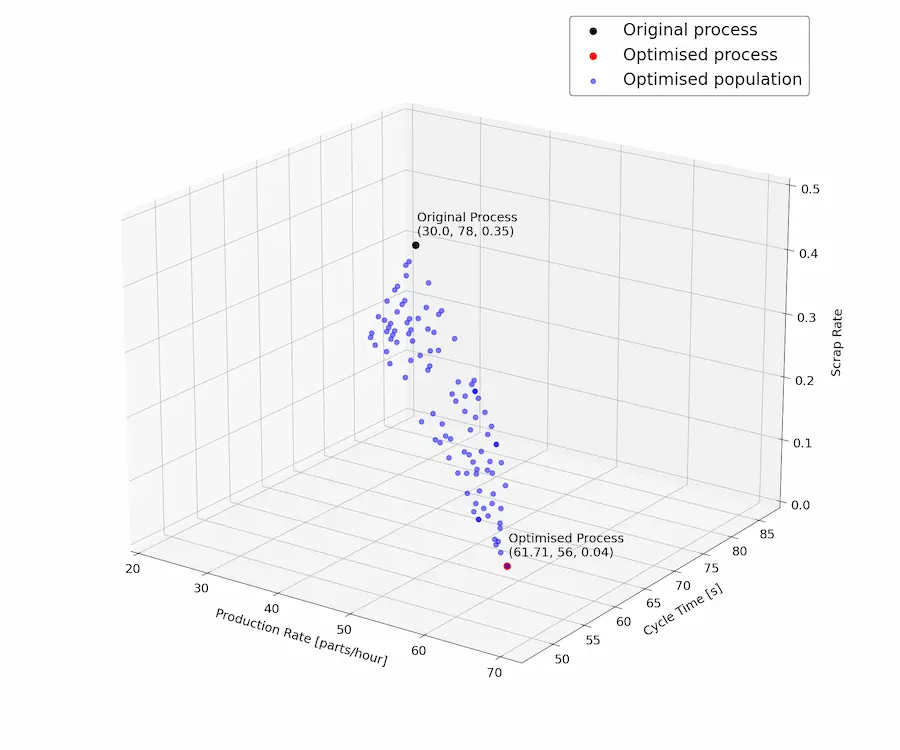
Hopper continuously tracks the influencing variables of the injection molding process and uses a (virtual) quality label to continuously adjust the optimization models according to the situation.
This means that it is also possible to react to changing conditions, such as new products or new materials. The models are transferable to the same machines.
= Continuous reduction and stabilization of scrap rate and cycle time
Closed-loop optimization through automatic parameter adjustment
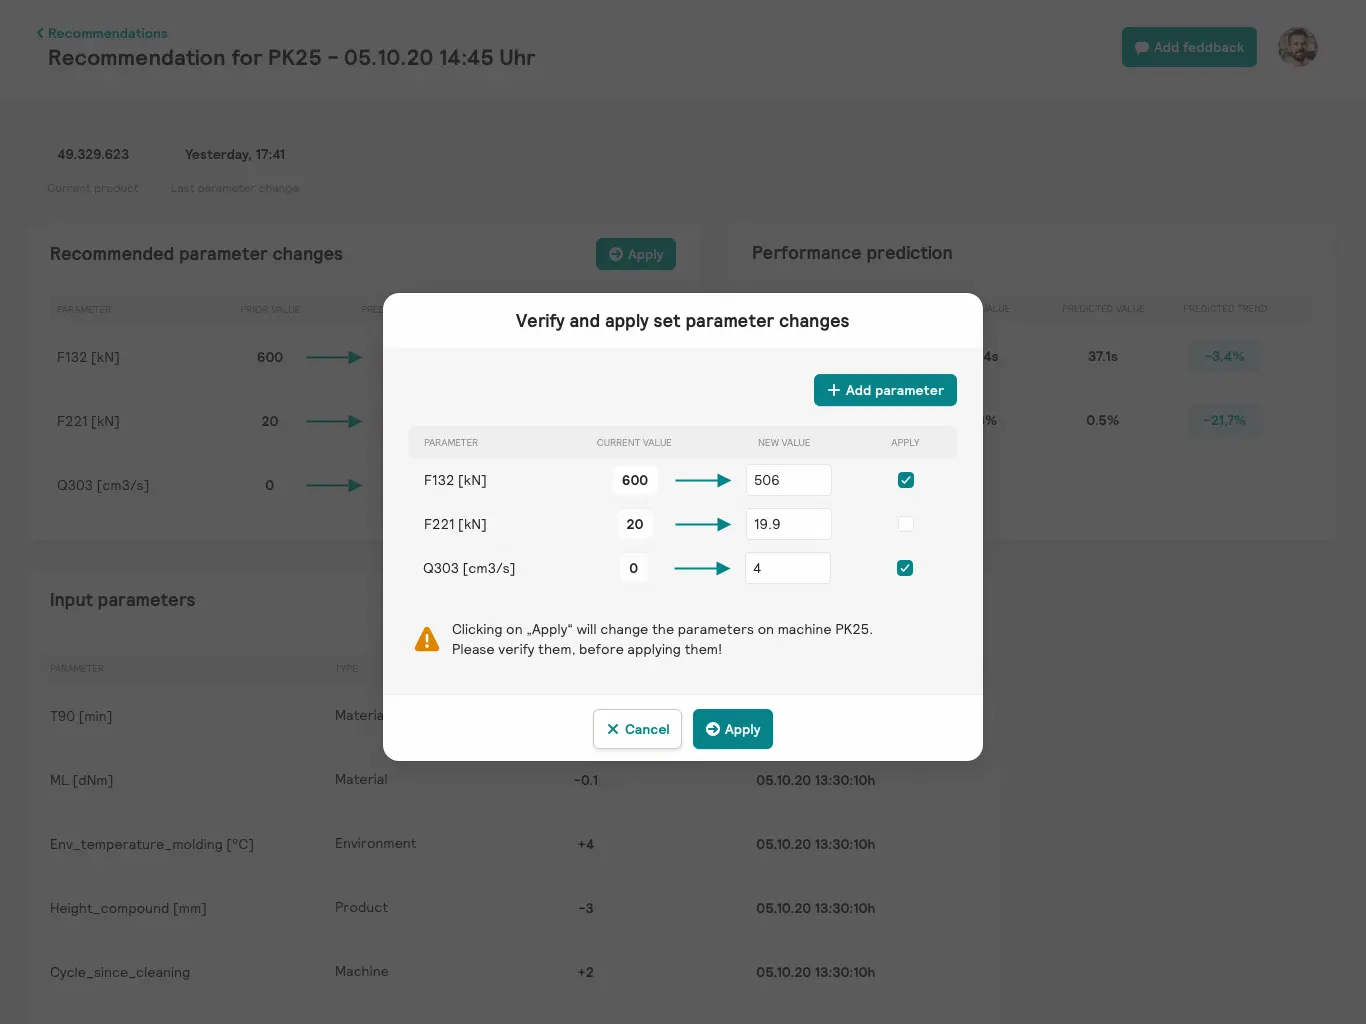
Apply parameter adjustment suggestions directly - Hopper writes the parameters directly to the machine controller.
This eliminates the need for manual adjustment by a machine operator.
- Automatic application of parameter adjustments
- Verification by user required
= Reduction of the operating effort of injection molding machines
The Value of Hopper

5-20%
Reduction of rejects

Up to 20%
Reduction of the cycle time or process phase

10 - 30%
Extension of the multi-machine operation
Hopper solves these production problems
- Optimal set parameter s in elastomer and thermoplastic injection molding, as well as for materials that are difficult to process, such as those with high recycled content
- Adaptive response to fluctuations in raw material batches, e.g., due to variations in drying, temperature, MFI changes, the use of recycled materials (PCR), or different elastomer batches
- Simplification of multi-machine operation through situational suggestions for all connected machines
All features of Hopper

Set parameter optimization
Set parameter optimization
Hopper continuously analyzes the influencing variables of the injection molding process and suggests situational adjustments to set parameter - with the aim of keeping scrap and cycle time as low as possible.
- Consideration of material, process and environmental data
- Receive recommendations in the browser or on a mobile device via push message

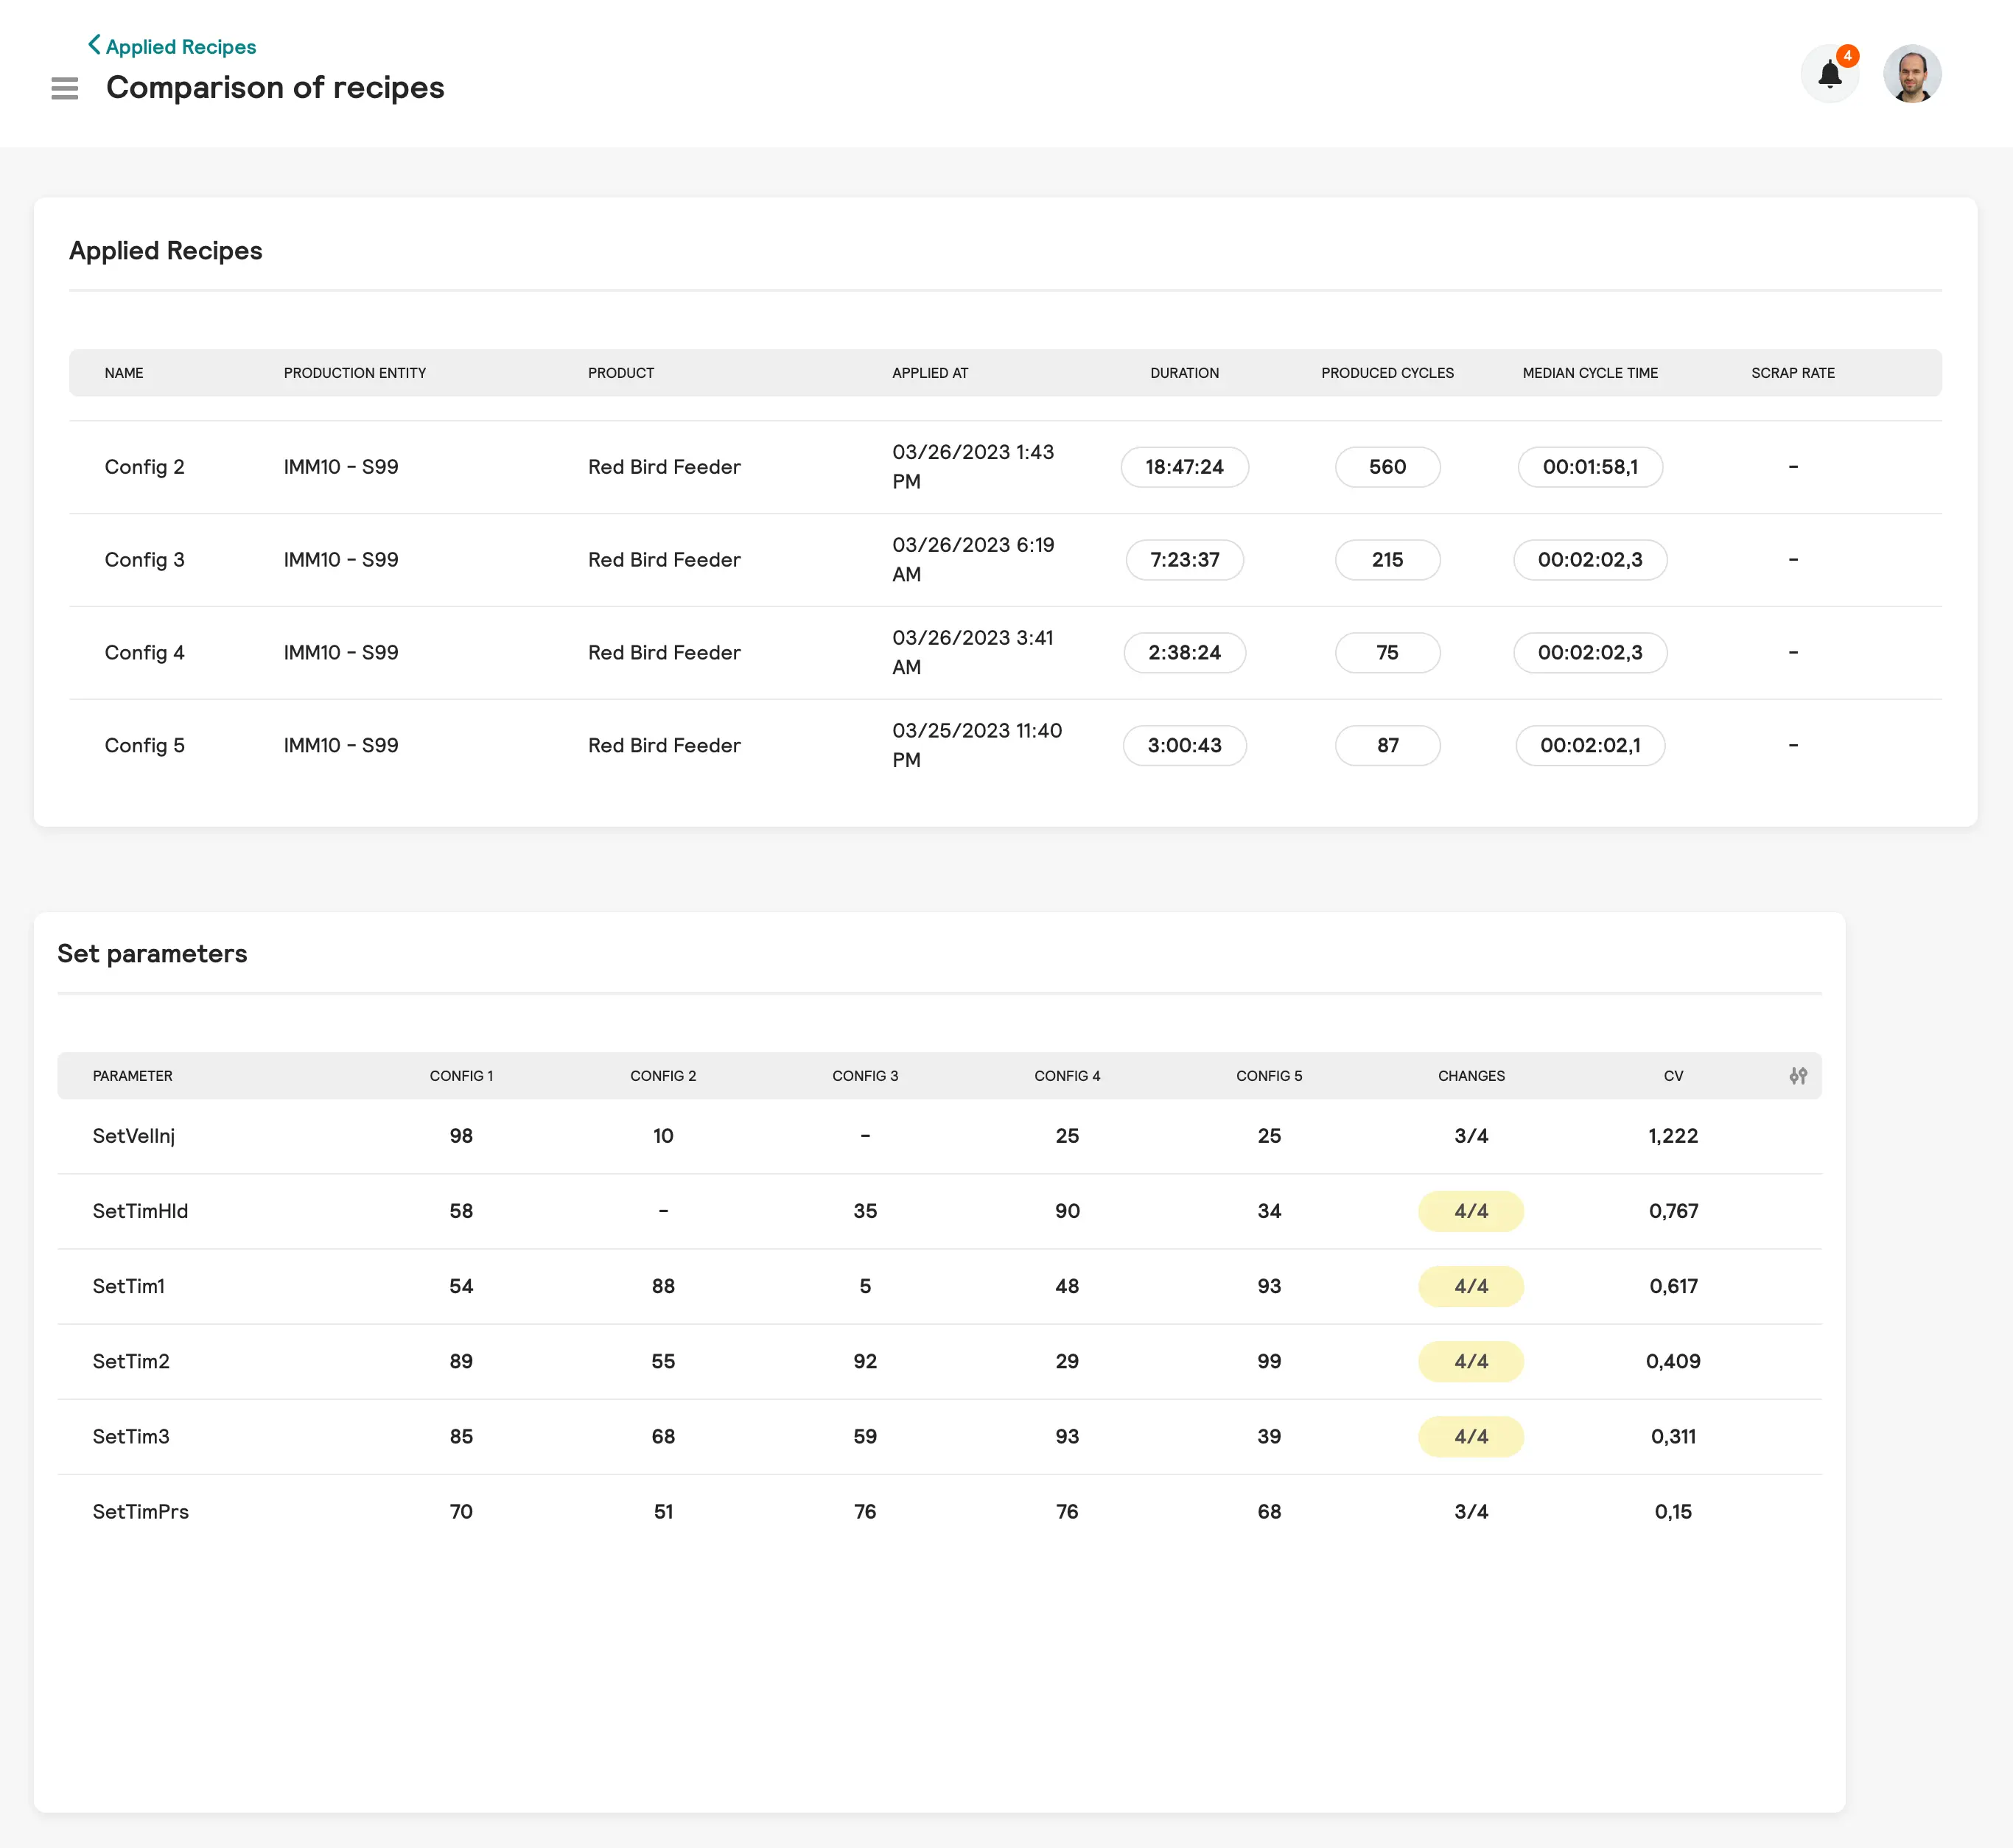
Recipe comparison
Recipe comparison
Compare applied recipes in terms of KPIs and different setting parameters.
Get an overview of which recipes worked and how well.

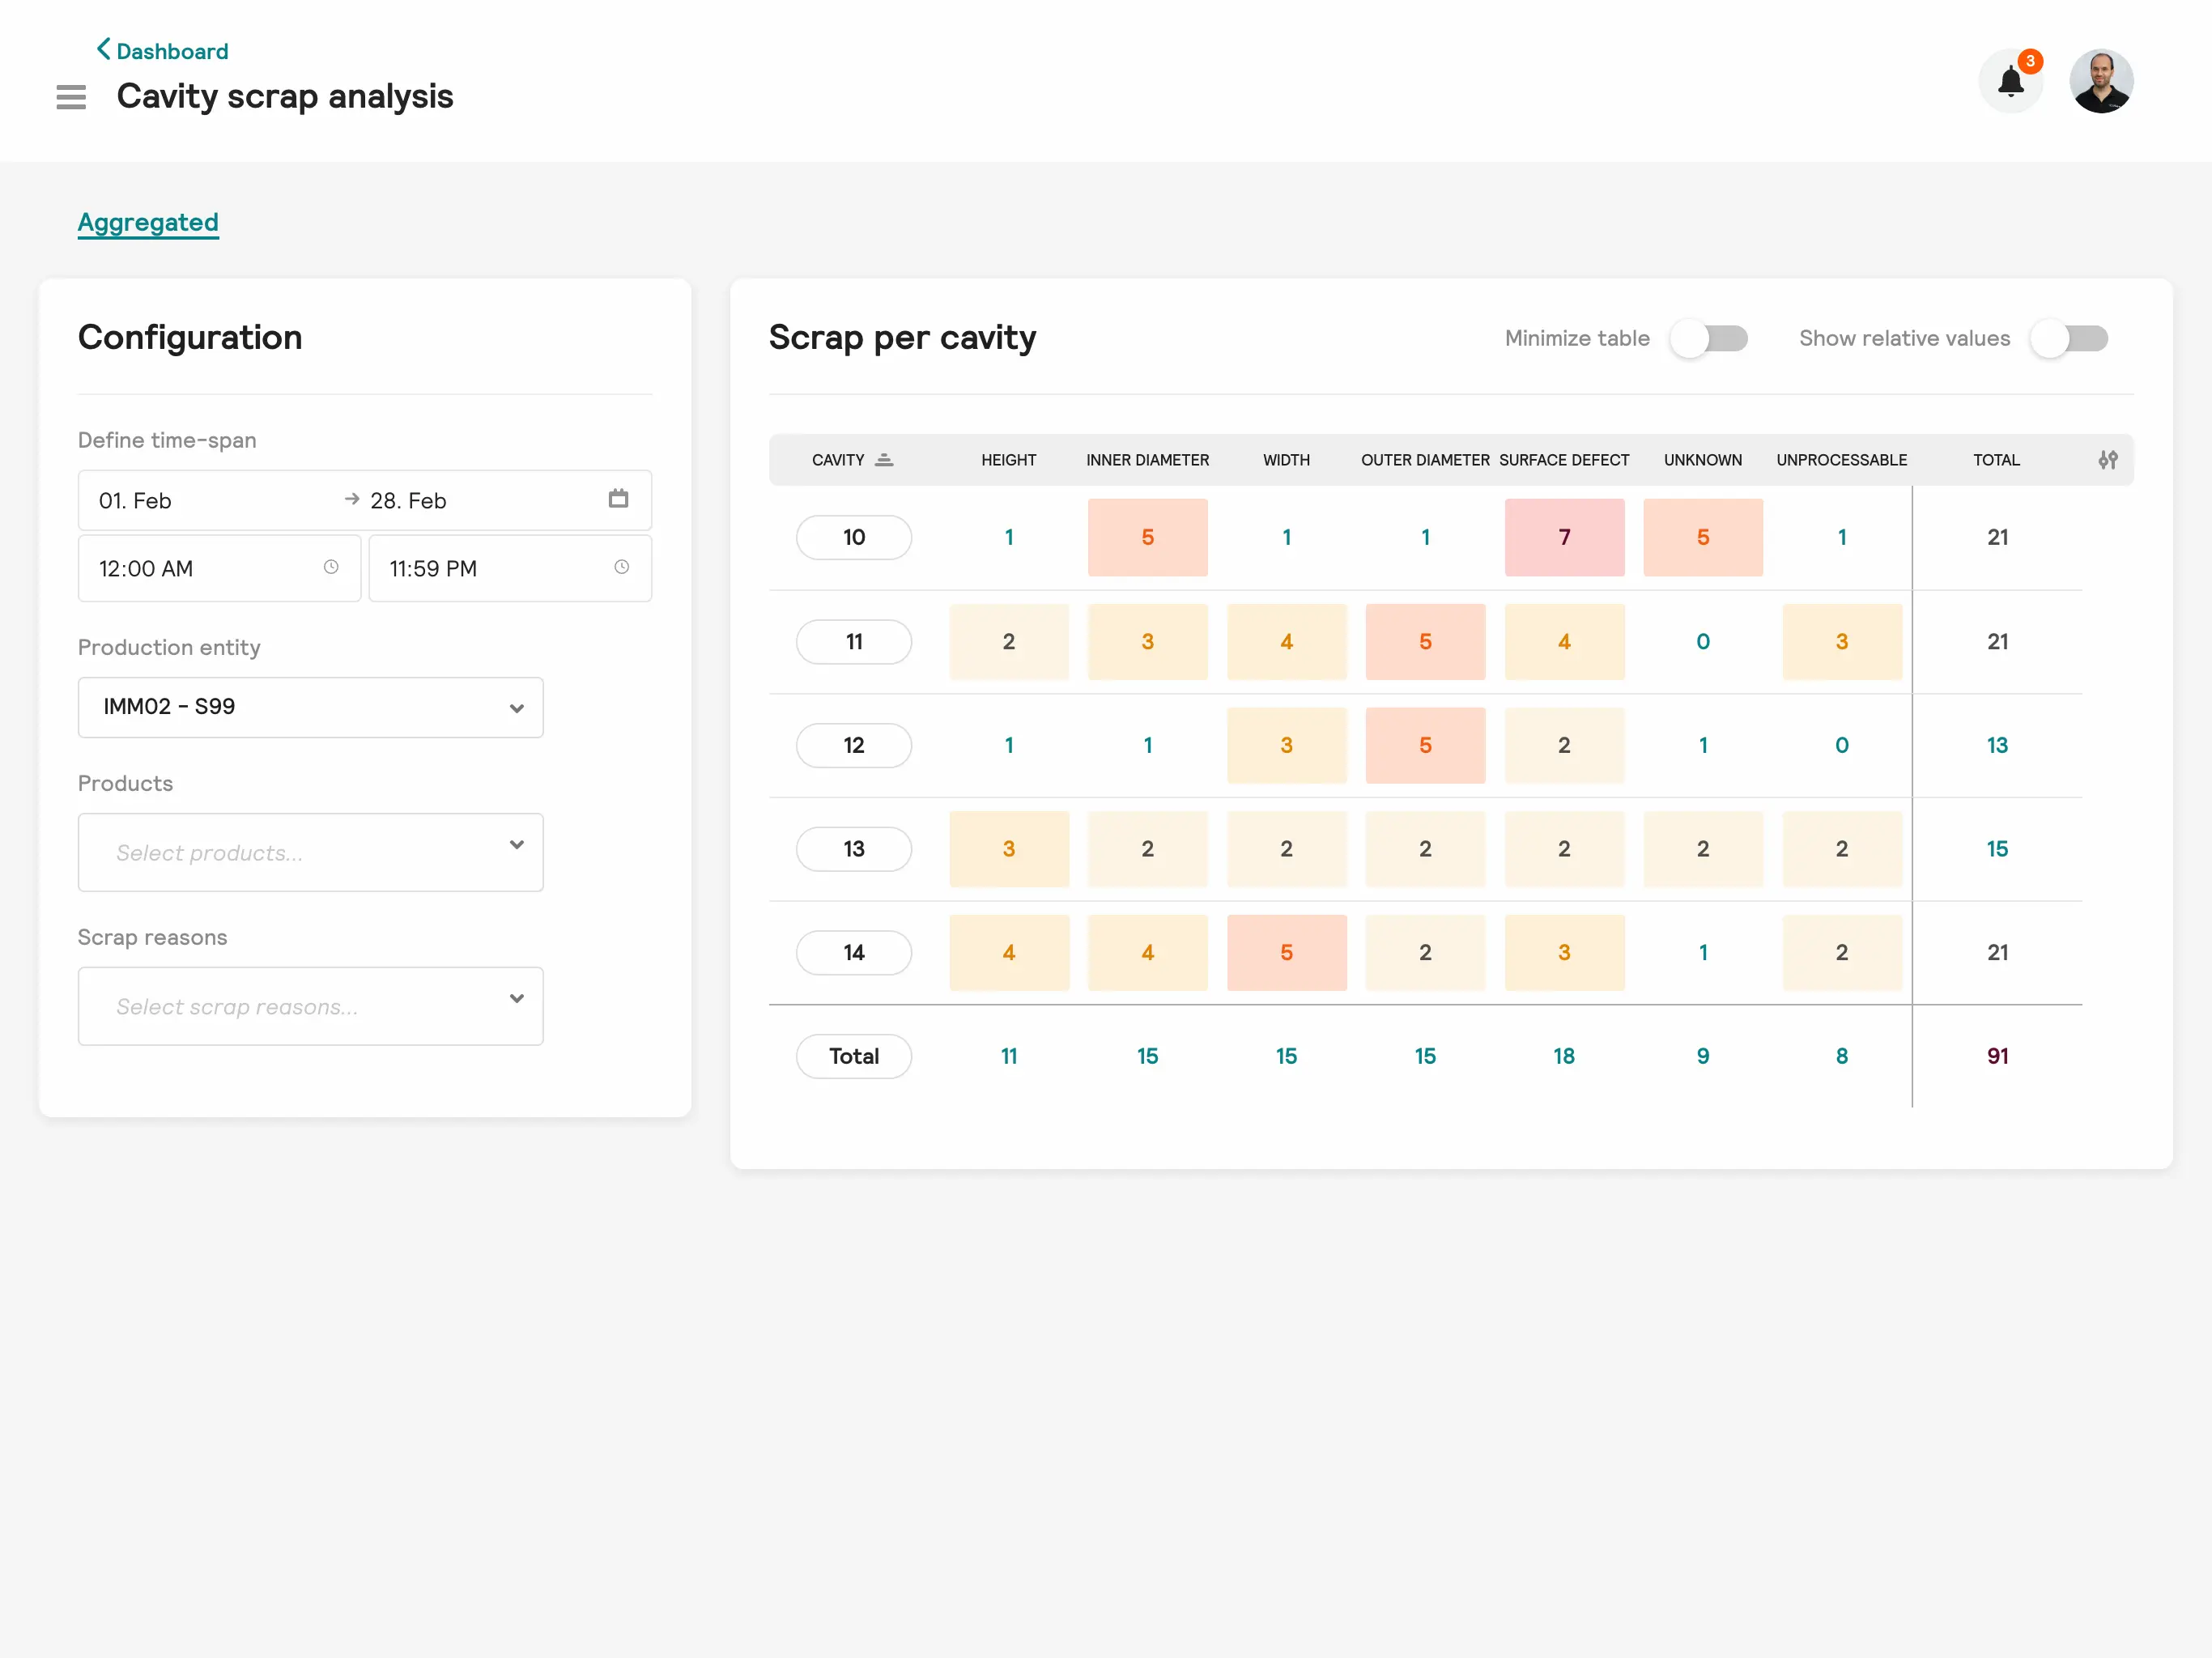
Scrap evaluation
Scrap evaluation
Analyze rejects occurring in the injection molding process, broken down by reason for rejection and cavity.
This allows you to precisely identify problem areas and initiate optimization measures with precision.

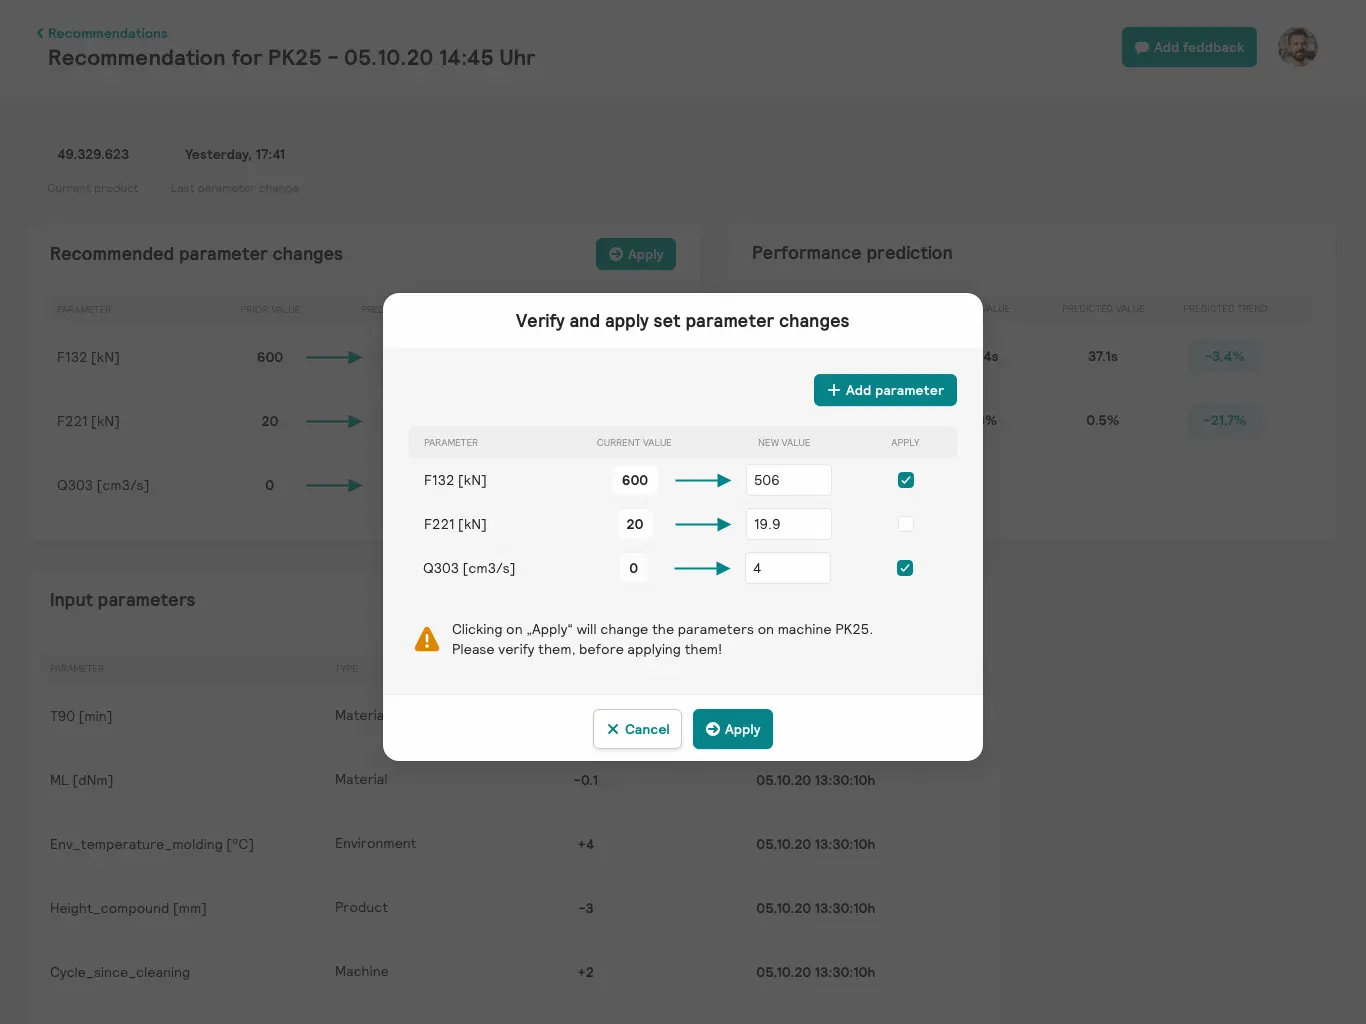
Automatic application of parameter adjustments
Automatic application of parameter adjustments
Apply parameter adjustment suggestions directly - Hopper writes the parameters directly to the machine controller.
This eliminates the need for manual adjustment by a machine operator.
- Automatic application of parameter adjustments
- Verification by user required

Parameter Notifications
Notification Settings
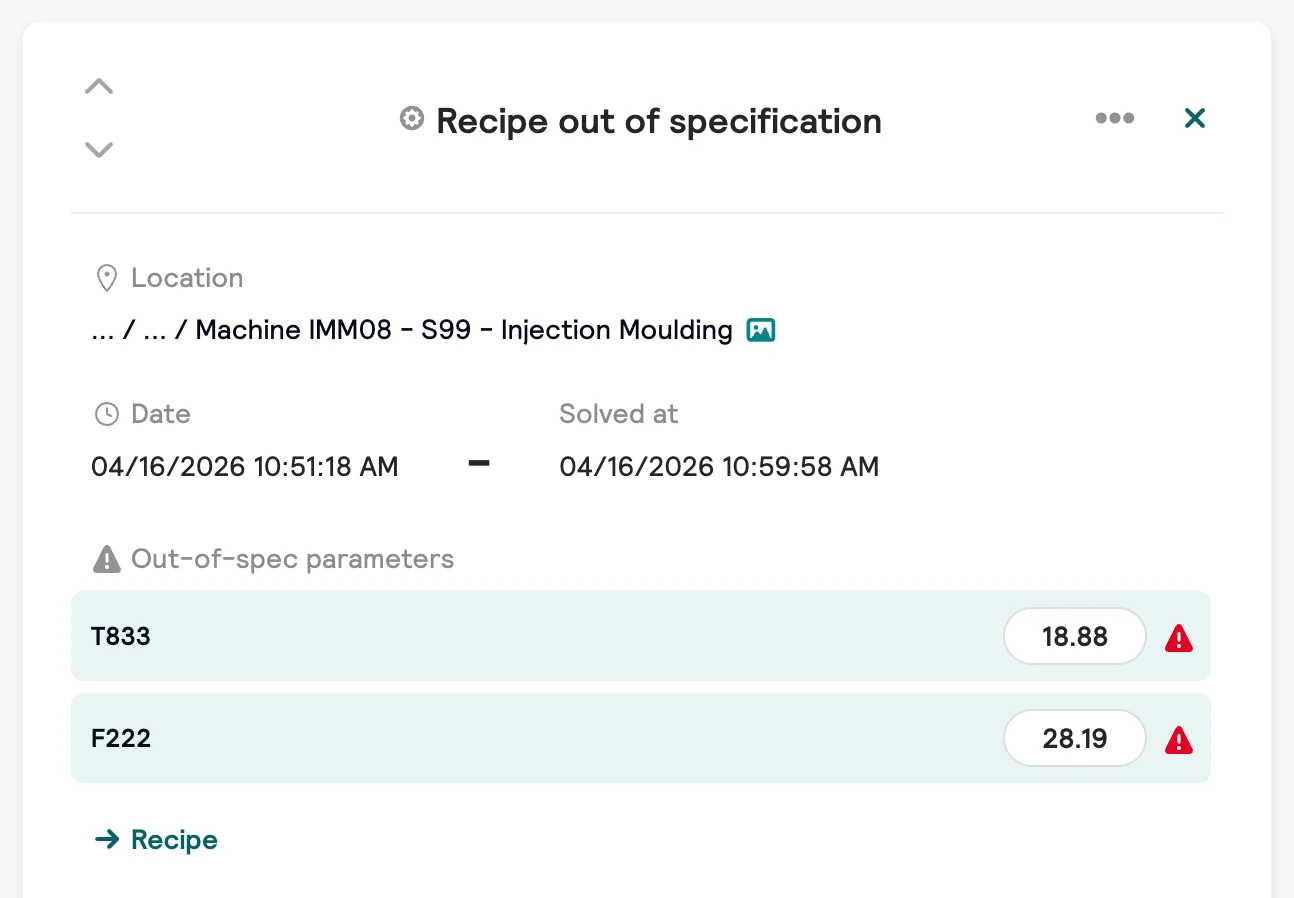
Hopper sends an alert as soon as a parameter or measured value goes outside its defined range.
If a value falls outside the specified limits, the system sends a notification. The team responds immediately, rather than discovering the problem by chance.
Interface


Security


Add-ons


What our customers & partners say
Hopper at ZAHORANSKY Automation & Molds
"Hopper analyzes combined machine and material data for us over the last three months, which provides transparency that we didn't have before. The ad hoc evaluation is particularly helpful for difficult materials such as COC or COP. The AI provides specific counterproposals, which saves a tremendous amount of time and waste."
Sven Walz, injection molding process expert at ZAHORANSKY
20% shorter ramp-ups and 10-17% less waste during production start-up

Hopper at Freudenberg Sealing Technologies
"The plus10 Hopper runs with its parameter suggestions on our injection molding machines and ensures higher output. It supports our setup engineers in fine-tuning machine settings and troubleshooting specific problems to increase and stabilize efficiency across all shifts in our complex elastomer injection molding processes."
Andrea Botta, Process Engineering Manager at Freudenberg Sealing Technologies
Increased and more stable output across all shifts, as well as shorter setup times

Hopper at ZAHORANSKY Automation & Molds
"Hopper analyzes combined machine and material data for us over the last three months, which provides transparency that we didn't have before. The ad hoc evaluation is particularly helpful for difficult materials such as COC or COP. The AI provides specific counterproposals, which saves a tremendous amount of time and waste."
Sven Walz, injection molding process expert at ZAHORANSKY
20% shorter ramp-ups and 10-17% less waste during production start-up
Contact now
- Personal Product Presentation with Live Demo
- Initial Assessment of Your Use Case
- Help with Calculating Your ROI
More products from plus10


Do you have questions? We have answers.
And if you have any further questions, please feel free to contact us.

The machine's internal control system essentially keeps the shot weight constant. In addition, Hopper responds to environmental influences and changes in the raw material within the specified parameter windows and addresses complex defect patterns such as optical defects (e.g., burn marks or streaks), dimensional accuracy, warpage, and black spots.
Machine-integrated dynamic/learning functions typically rely exclusively on the control data from the respective machine. Hopper not only uses high-frequency machine data from all connected machines (not just a single one), but also contextual information such as the raw material properties of the respective batch and environmental conditions. This enables Hopper to perform transfer learning: Since the software is compatible with different machine types and manufacturers in injection molding, data can be combined and compared across the entire machine fleet.
Machine-integrated functions in injection molding machines are limited to the transition point and the holding pressure phase. Hopper, on the other hand, provides optimized profiles for the plasticizing, injection, and holding pressure phases—so it not only shifts the transition point but also optimizes the entire process sequence. A recommendation can include up to 70 parameters—significantly more than with machine-integrated functions, which aim for consistent weight or volume from shot to shot. Hopper ensures minimal process changes and avoids “fluctuations” within the permissible process window.
Machine-integrated dynamic functions are designed to maintain a constant shot weight or volume despite fluctuations in viscosity or density—both of which are difficult to control. Hopper optimizes the combination of cycle time and scrap rate (good-part yield per hour as the optimization target), taking into account various causes of scrap such as dimensional deviations, surface defects, flow lines, and mechanical properties.
Machine-integrated functions intervene during the current cycle. Hopper, on the other hand, does not intervene until the current cycle is complete—that is, no earlier than the next cycle.
Machine-integrated functions prevent in-process scrap during production that results from fluctuations in shot weight.
Hopper:
- Faster tool changes thanks to recommendations for “Shot 1” that are already tailored to the current raw material batch and environmental conditions—no manual readjustment is necessary
- Prevention of in-process scrap caused by process fluctuations or changes in boundary conditions (climate/dryer/material batch)
- Compliance check to verify that parts were produced within validated parameter windows
The hopper increases the yield of good parts produced per hour, for example in elastomer and thermoplastic injection molding, as well as when processing difficult-to-process materials, such as those with high recycled content.
Hopper provides a parameter suggestion for the very first cycle following a tool or material change (“Cycle 0”), which is automatically tailored to the current raw material batch and environmental conditions. Manual, experience-based setup—which, depending on the material and the team’s routine, can currently take anywhere from a few minutes to several hours—is largely eliminated. This not only shortens setup time but, more importantly, keeps it consistently and reliably short, regardless of the individual’s experience.
Hopper typically learns for 6–8 weeks using live data from the running plant (“Silent Mode”) without disrupting the process through explicit test sequences (DoE). From the go-live date onward, the quality of the recommendations continues to improve as the system continuously learns.
Licensing is provided as an annual subscription per connected injection molding machine, including the necessary cloud computing power, storage, and support. Separate from this are the one-time configuration—which includes, among other things, the integration of various data sources—as well as one-time IT costs, depending on your existing IT infrastructure. The initial configuration and training are carried out in collaboration with an internally selected key user. All subsequent configurations can typically be performed independently by the key user.